Identify the product and exposure
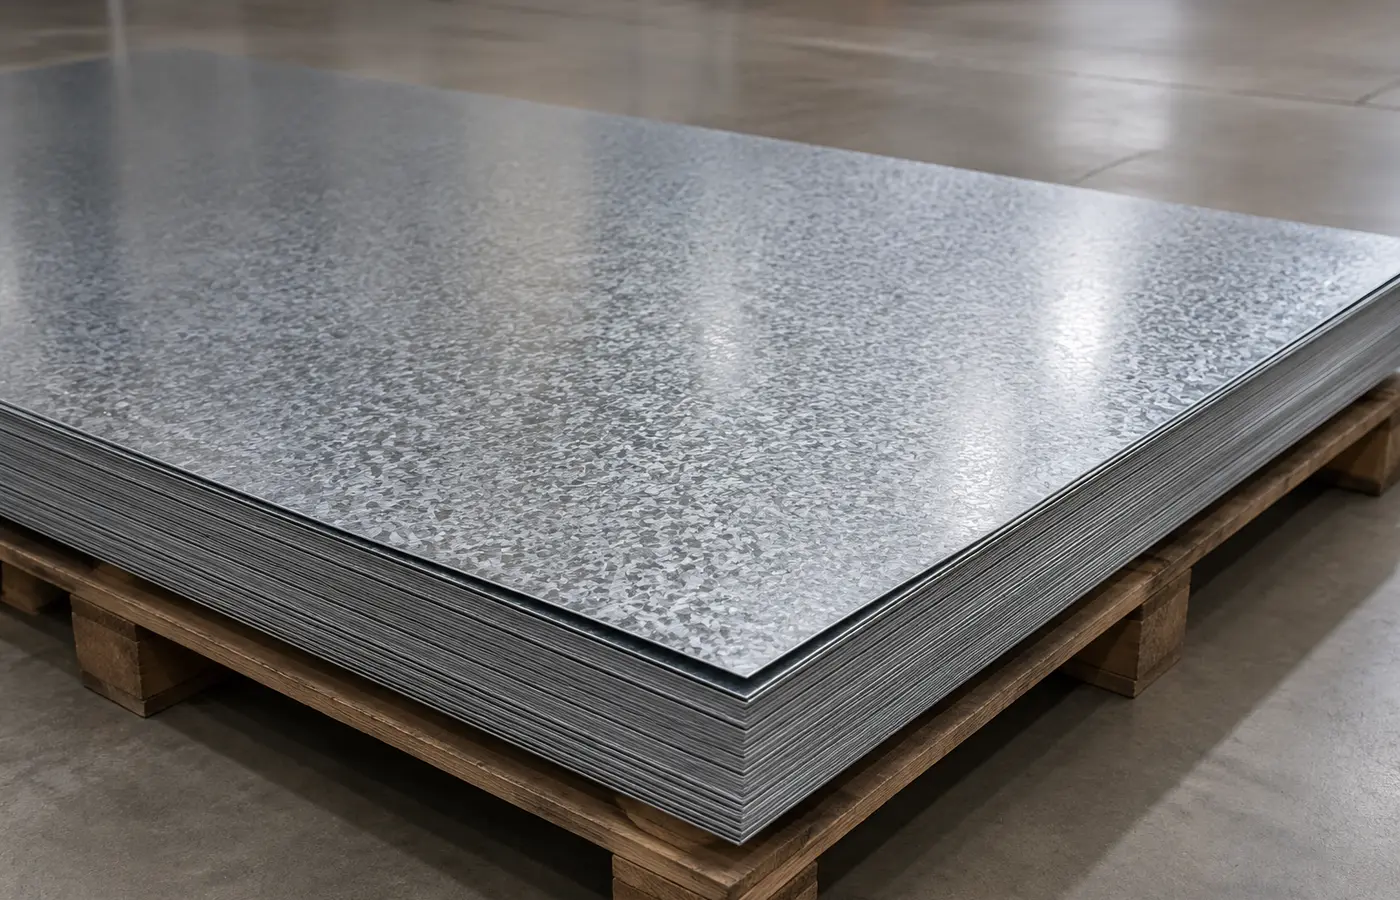
Not every metallic-coated sheet is the same. Confirm coating type, surface treatment, thickness and any paint system before selecting tools or repair materials.
Map whether the cut edge will remain dry, face condensation or salt, sit in a lap or contact another metal. Follow the exact supplier document rather than transferring instructions between coating families.
Work from one reference edge
Establish a datum, verify squareness and complete the flat pattern for bends, laps and holes before cutting. Mark face, direction and part number with a compatible method.
Dry-fit the first part before using it as a template. Kerf, shear clearance, blade condition and sheet movement can all change finished dimensions.
Limit unnecessary heat
Use a suitable shear, nibbler or approved mechanical method for the geometry and thickness. Check the first edge for burr, roll-over and coating lift.
Do not choose grinding or thermal cutting solely for speed. Heat and sparks can damage the zinc and finished surface, while hot work needs specific ventilation and fire controls.
Guard and support the work
Support both sides of the cut and control the offcut. OSHA identifies guillotine cutters and shears as machines requiring point-of-operation guarding.
Use task-appropriate eye, face and cut protection, and isolate energy before adjustment, blade changes or clearing jams.
Deburr without stripping sound coating
Remove only the sharp projection; broad abrasive grinding needlessly removes intact zinc. Inspect tears, folded metal and coating lift instead of hiding them with paint.
Clean the edge of loose particles and cutting oil before any repair coating is applied.
Remove swarf promptly
Steel swarf left on coated sheet can rust, stain and scratch the surface. Inspect laps, valleys and film edges as well as open flat areas.
Use a soft brush, suitable vacuum or supplier-approved method. Remove any fluid that is incompatible with later paint, sealant or adhesive.
Protect the cut edge for its environment
Adjacent zinc can offer sacrificial protection to small exposed areas, but performance depends on coating, steel thickness, exposure and drying. Do not treat a specialist zinc-aluminium-magnesium claim as a guarantee for ordinary galvanized sheet.
Where repair is required, clean the edge and apply the supplier-specified compatible zinc-rich or coating system. Correct water traps and drainage rather than relying on touch-up alone.
Approve and record the first piece
Measure dimensions, diagonals, edge straightness and burrs, then trial-fit the real assembly. Record machine, tool, settings and repair product.
During the batch, monitor burr growth, scratches and swarf removal. Pack only clean, dry parts after the repair system has cured as instructed.